October 31, 2026 · Indumor
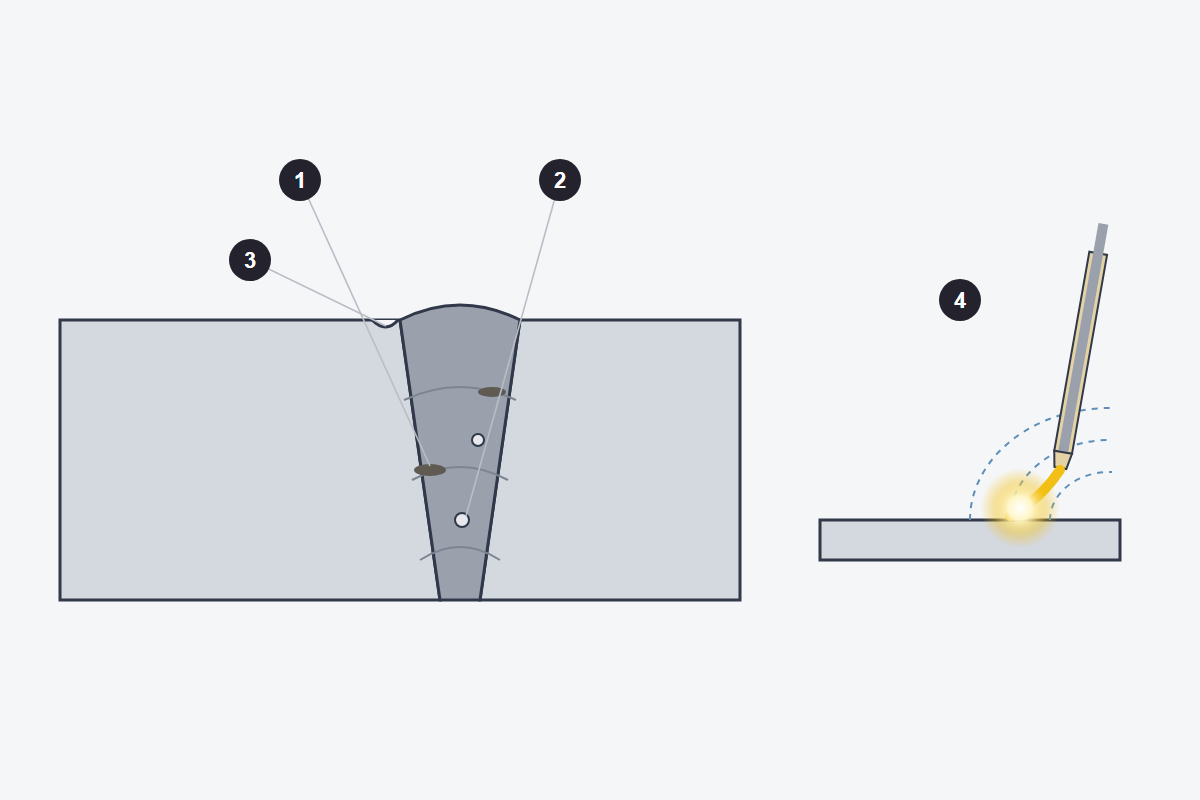
On the left, in the cross-section of a multipass joint: 1 slag trapped between passes, 2 porosity, 3 undercut. On the right, 4 the arc deflected by arc blow near the end of the plate.
Slag inclusion: a non-metallic particle trapped inside the weld. In stick welding, the defect that best gives away a rush job. Together with arc blow and start porosity, it makes up the trio of problems that keeps coming back with this process. Why so many? Because the electrode leaves slag, depends on the hand and often works on DC and outdoors. The list below sets them out with their cause and cure.
The list can go on the wall at the station, but half the cures start before striking the arc: dry rods, a clean joint and a well-placed clamp. The other half is craft, and it is earned on test plates.
The slag also reports back. If it peels off by itself on a rutile rod, the settings are right; if it sticks along the edges, there is usually undercut hiding underneath, worth checking before the next pass.
In practice, one habit sums up the lesson: a pass left uncleaned is a pass done twice. If you have joints that must pass inspection, Indumor welds them with that care, and the quote costs nothing.
Think of the answer before you open it.
Poor cleaning between passes, grooves that hide slag, too little current or an angle that lets the slag run ahead of the pool.
The deflection of the arc by its magnetic field on DC, near edges, plate ends and the clamp. It is corrected by switching to AC, moving the clamp, tacking and tilting the rod against it.
From striking on the cold crater; it is avoided by striking ahead of the crater and coming back.
Grind it out and check it, because it leaves a hard spot with microcracks.
We weld them cleaning every pass and with the right electrode.
© Indumor 2010–2026 — Industrial steel fabrication, Córdoba, Argentina
