October 31, 2026 · Indumor
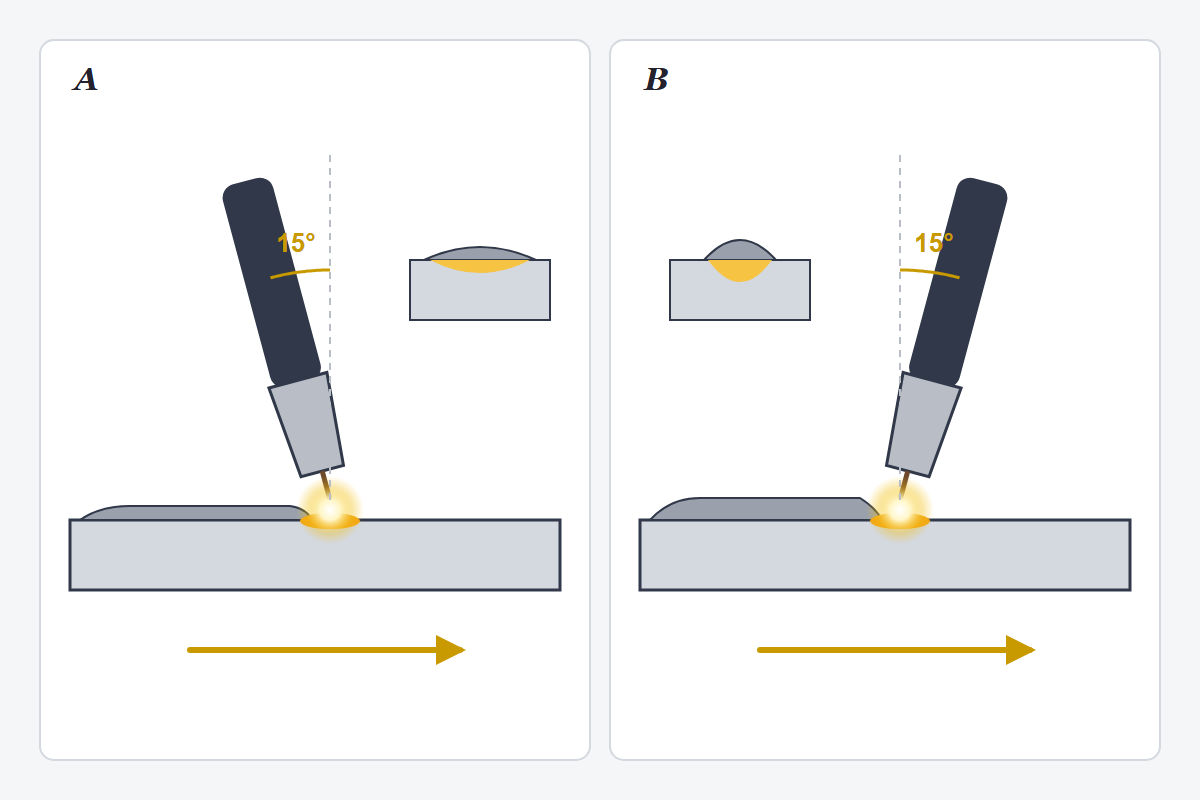
Starting values for carbon steel with ER70S-6 wire and an argon-CO₂ blend (M21), in the flat or horizontal position, with about 12 to 15 mm of contact tip to work distance in short-circuit and 18 to 20 mm in spray. They are a starting point: fine-tune them on a scrap plate of the same thickness and, when there is a procedure, the WPS rules.
| Thickness | Joint | Wire (mm) | Wire feed speed, m/min (ipm) | Voltage (V) | Approx. current (A) | Transfer | Gas, L/min (CFH) |
|---|---|---|---|---|---|---|---|
| 1 mm (20 ga) | Butt or fillet | 0.8 | 3 to 4 (120 to 160) | 15 to 16 | 60 to 80 | Short-circuit | 10 (21) |
| 2 mm (14 ga) | Butt or fillet | 0.8 or 1.0 | 3.5 to 4.5 (140 to 180) | 16 to 18 | 90 to 110 | Short-circuit | 10 to 12 (21 to 25) |
| 3 mm (1/8 in) | Fillet or gapped butt | 1.0 | 4.5 to 6 (180 to 240) | 17 to 19 | 110 to 140 | Short-circuit | 10 to 12 (21 to 25) |
| 4 to 5 mm (3/16 in) | Fillet | 1.0 | 6 to 8 (240 to 315) | 19 to 21 | 140 to 180 | Short-circuit | 12 (25) |
| 6 mm (1/4 in) | Fillet in PB (2F) | 1.2 | 6 to 7 (240 to 275) | 23 to 26 | 200 to 230 | Globular to spray, depending on blend | 12 to 15 (25 to 32) |
| 8 to 10 mm (3/8 in) | Fillet or V, multipass | 1.2 | 8 to 10 (315 to 395) | 27 to 30 | 250 to 290 | Spray | 15 (32) |
| 12 mm (1/2 in) and up | V or double V, multipass | 1.2 | 9 to 12 (355 to 470) | 28 to 32 | 270 to 320 | Spray | 15 to 18 (32 to 38) |
Each column is explained in lesson 4, lesson 5 and lesson 8 of the course. The chart belongs to the Steel Knowledge Hub of Indumor; for section sizes and weights, see the technical tables.
We quote the welding with the procedure each joint needs.
© Indumor 2010–2026 — Industrial steel fabrication, Córdoba, Argentina
